About Best Air

Two decades of engineering excellence in industrial air handling solutions.

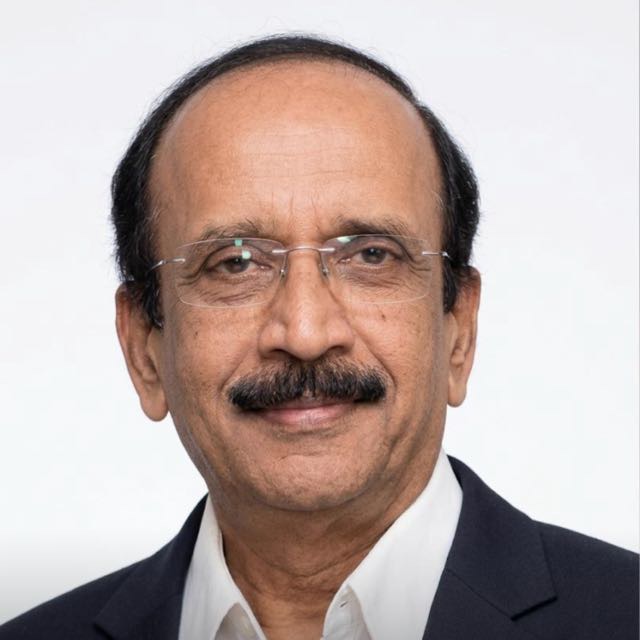
Mr. Jerrome Sudakar – Founder & Managing Director

Jerrome Sudakar

Founder & Managing Director – Bestair Group of Companies

Mr. Jerrome Sudakar is a Textile Technocrat and accomplished entrepreneur with over four decades of experience in the textile, textile machinery, engineering, and industrial air-conditioning sectors.

He completed his Textile Technology degree from the Institute of Technology, Adyar, Chennai during 1975–1978 and subsequently completed his Postgraduate Programme in Management from the University of Madras during 1986–1987.

He began his professional career in the early 1980s with leading textile organizations such as Sundararaja Mills and Madura Coats, followed by extensive experience with reputed textile machinery manufacturers including LMW, Inarco, Batliboi. His association with Binny Mills also provided valuable experience in the development of products for suiting, shirting, and furnishing applications.

Meet the Founder

With this strong and diversified industry background, Mr. Sudakar founded Best Air Systems Pvt. Ltd. and subsequently Best Air Engineering (India) Pvt. Ltd. Under his leadership, the Bestair Group has specialized in the design, engineering, manufacturing, installation, and turnkey execution of humidification, ventilation, and air-conditioning systems, particularly for the textile industry.

Over the years, Bestair has successfully executed approximately 3,500 projects globally, including projects in Thailand, Egypt, Bangladesh, and other international markets. This extensive experience has enabled the company to develop a deep understanding of textile processes and the critical importance of maintaining precise temperature, humidity, and air-flow conditions for optimum production and quality.

Building on this expertise, Bestair is now introducing a new-generation air-conditioning concept exclusively for the textile industry, designed to maintain precise environmental conditions while adapting to varying ambient conditions across different geographical locations.

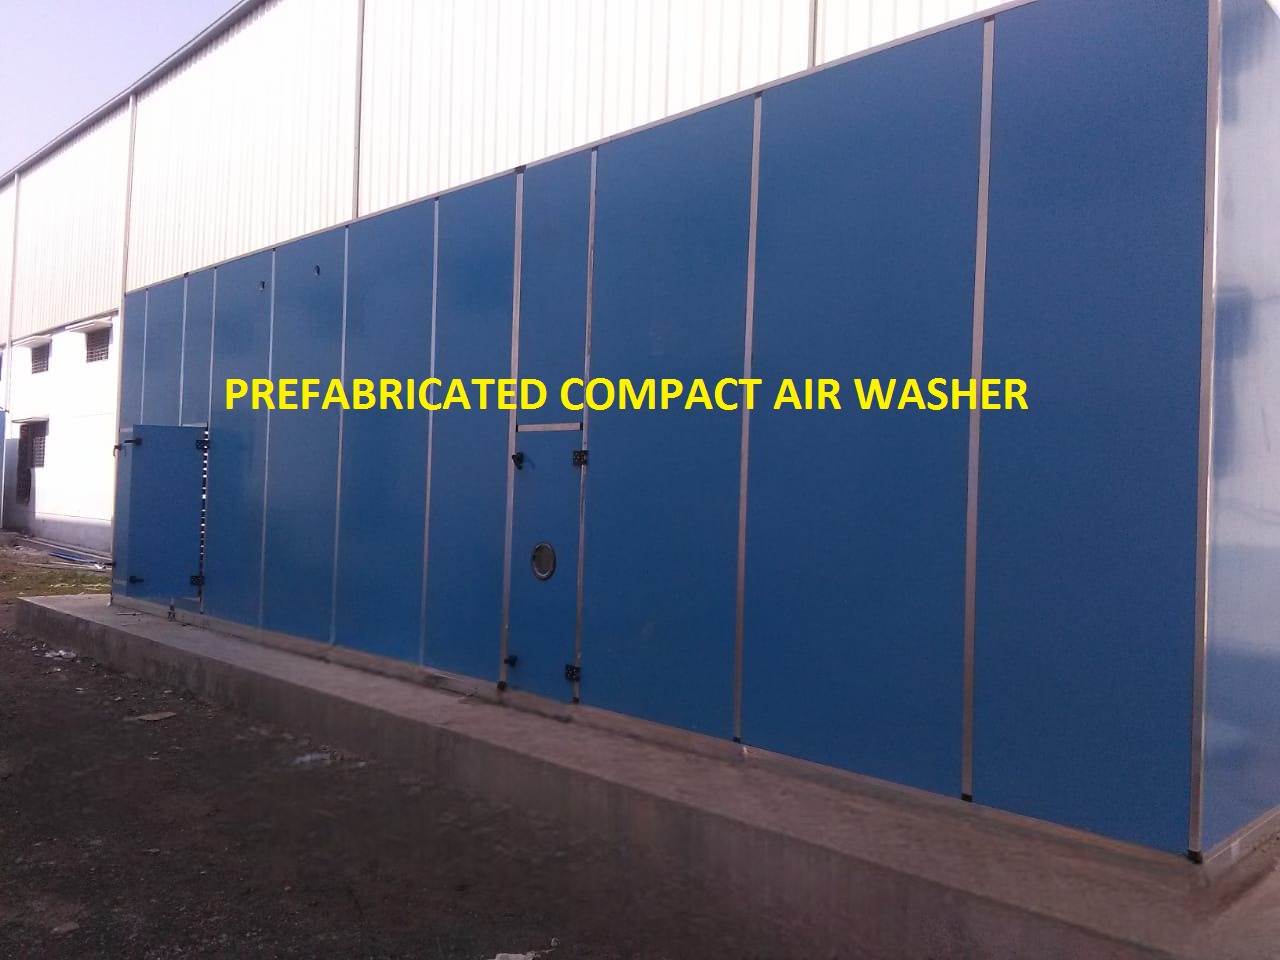
As part of this initiative, Bestair is developing prefabricated, fully automated air-conditioning units that offer economical investment, faster installation, reduced site work, reliable performance, precise temperature and humidity control, energy efficiency, and attractive ROI. These solutions are designed for textile projects ranging from smaller installations to capacities of up to 1 lakh spindles.

At Bestair, every project begins with a thorough understanding of the customer's process, machinery, plant configuration, production capacity, climatic conditions, environmental requirements, energy considerations, and future expansion plans. This enables the company to engineer solutions that are technically sound, commercially viable, easy to install, and designed for long-term performance.

With a unique combination of textile expertise, machinery knowledge, engineering experience, and global project exposure, Mr. Jerrome Sudakar continues to lead Bestair towards innovative, economical, and high-performance environmental control solutions for the textile industry.

BESTAIR – ENGINEERING THE RIGHT ENVIRONMENT FOR TEXTILE EXCELLENCE
Best Air Industrial Fan
20+ Years
3500+

Projects Completed

27+

Years Experience

Engineering the Air You Breathe

We are one of the trusted manufacturers of Humidification Systems, Exhaust Systems, and all types of industrial air management products.

We tailor solutions for textile mills, manufacturing units, commercial buildings and industrial working premises to enhance the overall operational efficiency, humidity control, ventilation, and air quality. We supply Mini Air Washers, Compact Air Washers, Civil Humidification Plants, Prefab Exhaust Plants, Civil Exhaust Plants, CDS Dust Collection Systems, Disc Filters, Drum Filters, Axial Flow Fans, Spray Nozzles, Mist Eliminators, Louvers, V Filters, Access Doors and PIR Ducting.

Manufactured with advanced technology and premium quality materials, our products are known for their durability, reliability, and high performance. Through our focus on quality, innovation and customer satisfaction, we provide customised solutions to industry standards to enable businesses to run efficiently, safely and sustainably.

Our Mission

To manufacture innovative, high-quality air management solutions that enhance industrial efficiency, safety, and performance.

Our Vision

To be a leading manufacturer recognised for engineering excellence, innovation, and customer satisfaction.

Our Values

We are driven by quality, integrity, innovation, reliability, and a commitment to exceeding customer expectations.

Our Promise

To deliver durable, efficient, and customised solutions with uncompromising quality, timely delivery, and dependable support.

Our Core Values

The principles that guide every product we build and every client we serve.

Quality First

Every component is sourced, fabricated, and tested to meet the highest industrial standards before leaving our facility.

Client Partnership

We don't just sell equipment — we build long-term relationships, supporting clients from site survey to commissioning and beyond.

Innovation

Continuously improving our designs to incorporate the latest in energy efficiency, materials, and airflow engineering.

Sustainability

Our evaporative cooling systems consume significantly less energy than conventional AC, reducing carbon footprint for our clients.

Reliability

Built for continuous industrial operation — our systems are engineered for minimal downtime and maximum uptime.

People-Centric

Better air quality means healthier, more productive workers. We engineer with human well-being at the core.

What Sets Us Apart

01

Deep Industry Expertise

Years of manufacturing experience delivering reliable solutions for diverse industrial applications.

02

End-to-End Custom Fabrication

Complete design, manufacturing, and customisation tailored to your project requirements.

03

Proven Track Record

Trusted by industries for delivering quality products and consistent performance.

04

Dedicated After-Sales Support

Responsive technical assistance and reliable service to ensure long-term satisfaction.

05

Energy-Efficient Designs

Engineered to reduce energy consumption while maximising operational efficiency.

06

On-Time Delivery

Efficient production and timely delivery to keep your projects on schedule.

Our Certifications

Backed by industry recognition and quality accreditations that reflect our commitment to engineering excellence.

Verified Certificate
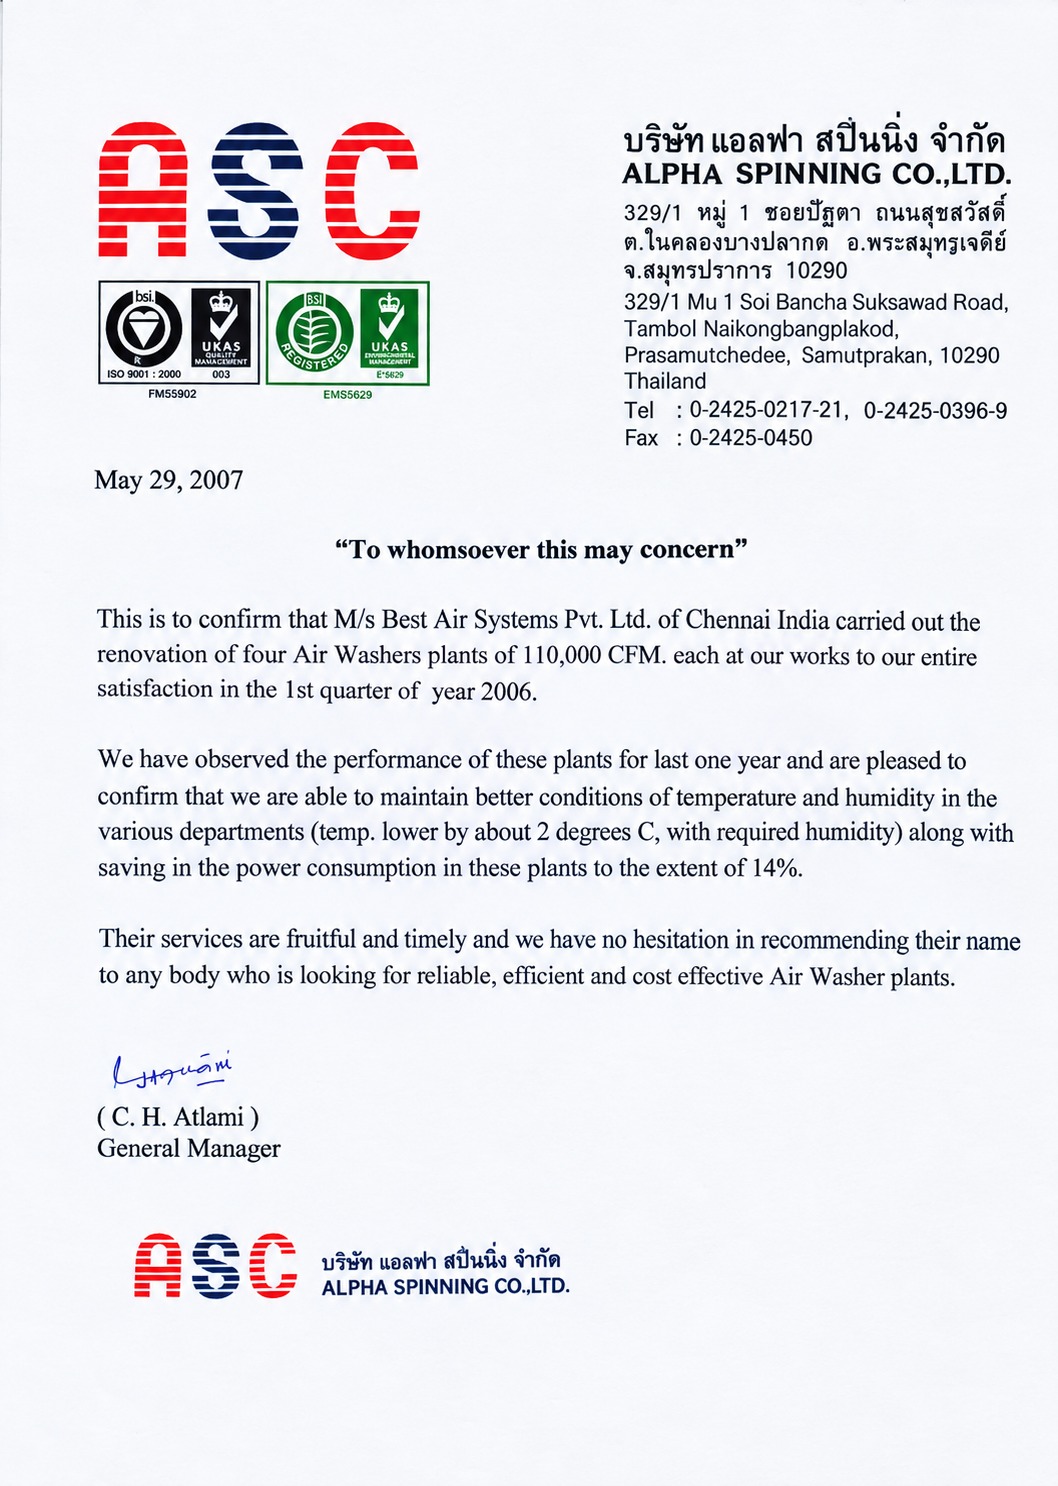
Best Air – Quality Certificate

Quality You Can Trust

Best Air Systems Pvt. Ltd. is a certified manufacturer of industrial air handling systems, recognised for maintaining the highest standards in product quality, engineering design, and manufacturing processes.

Our certifications reflect our unwavering dedication to delivering products that meet stringent industrial benchmarks. Every system we produce — from compact air washers to large-scale humidification plants — undergoes rigorous quality checks aligned with our certified standards.

Certified Manufacturing Facility

Our production plant operates under certified quality management protocols ensuring consistent product excellence.

Engineering Standards Compliance

All products are designed and tested to comply with applicable industrial and safety engineering standards.

Globally Recognised Quality

Trusted by clients across India and international markets including Thailand, Egypt, and Bangladesh.

Trusted by Leading Mills

Ramco MillsLoyal TextilesMontex NC JohnSubhalakshmi MillsCotton King Dilip FabricsSivajothiSJLT Neelam TextilesHi TechVel Tex LK TextileAarnavSabeena Ramco MillsLoyal TextilesMontex NC JohnSubhalakshmi MillsCotton King Dilip FabricsSivajothiSJLT Neelam TextilesHi TechVel Tex LK TextileAarnavSabeena

Ready to Work With Us?

Tell us about your project and we'll engineer the right solution for your plant.

Chat with us